COMMERCIAL AND INDUSTRIAL BOILER ECONOMIZERS
BOILER ECONOMIZERS
Tri-Tech Sales provides boiler economizers and flue gas heat recovery systems for commercial and industrial steam and hot water boiler applications. We represent Heatmizer, a manufacturer of boiler economizers engineered to recover heat from boiler exhaust and transfer that energy back into the system. A properly selected economizer can reduce stack temperature, improve overall boiler efficiency, lower fuel consumption, and recover energy that would otherwise leave through the boiler stack.
HOW A BOILER ECONOMIZER WORKS
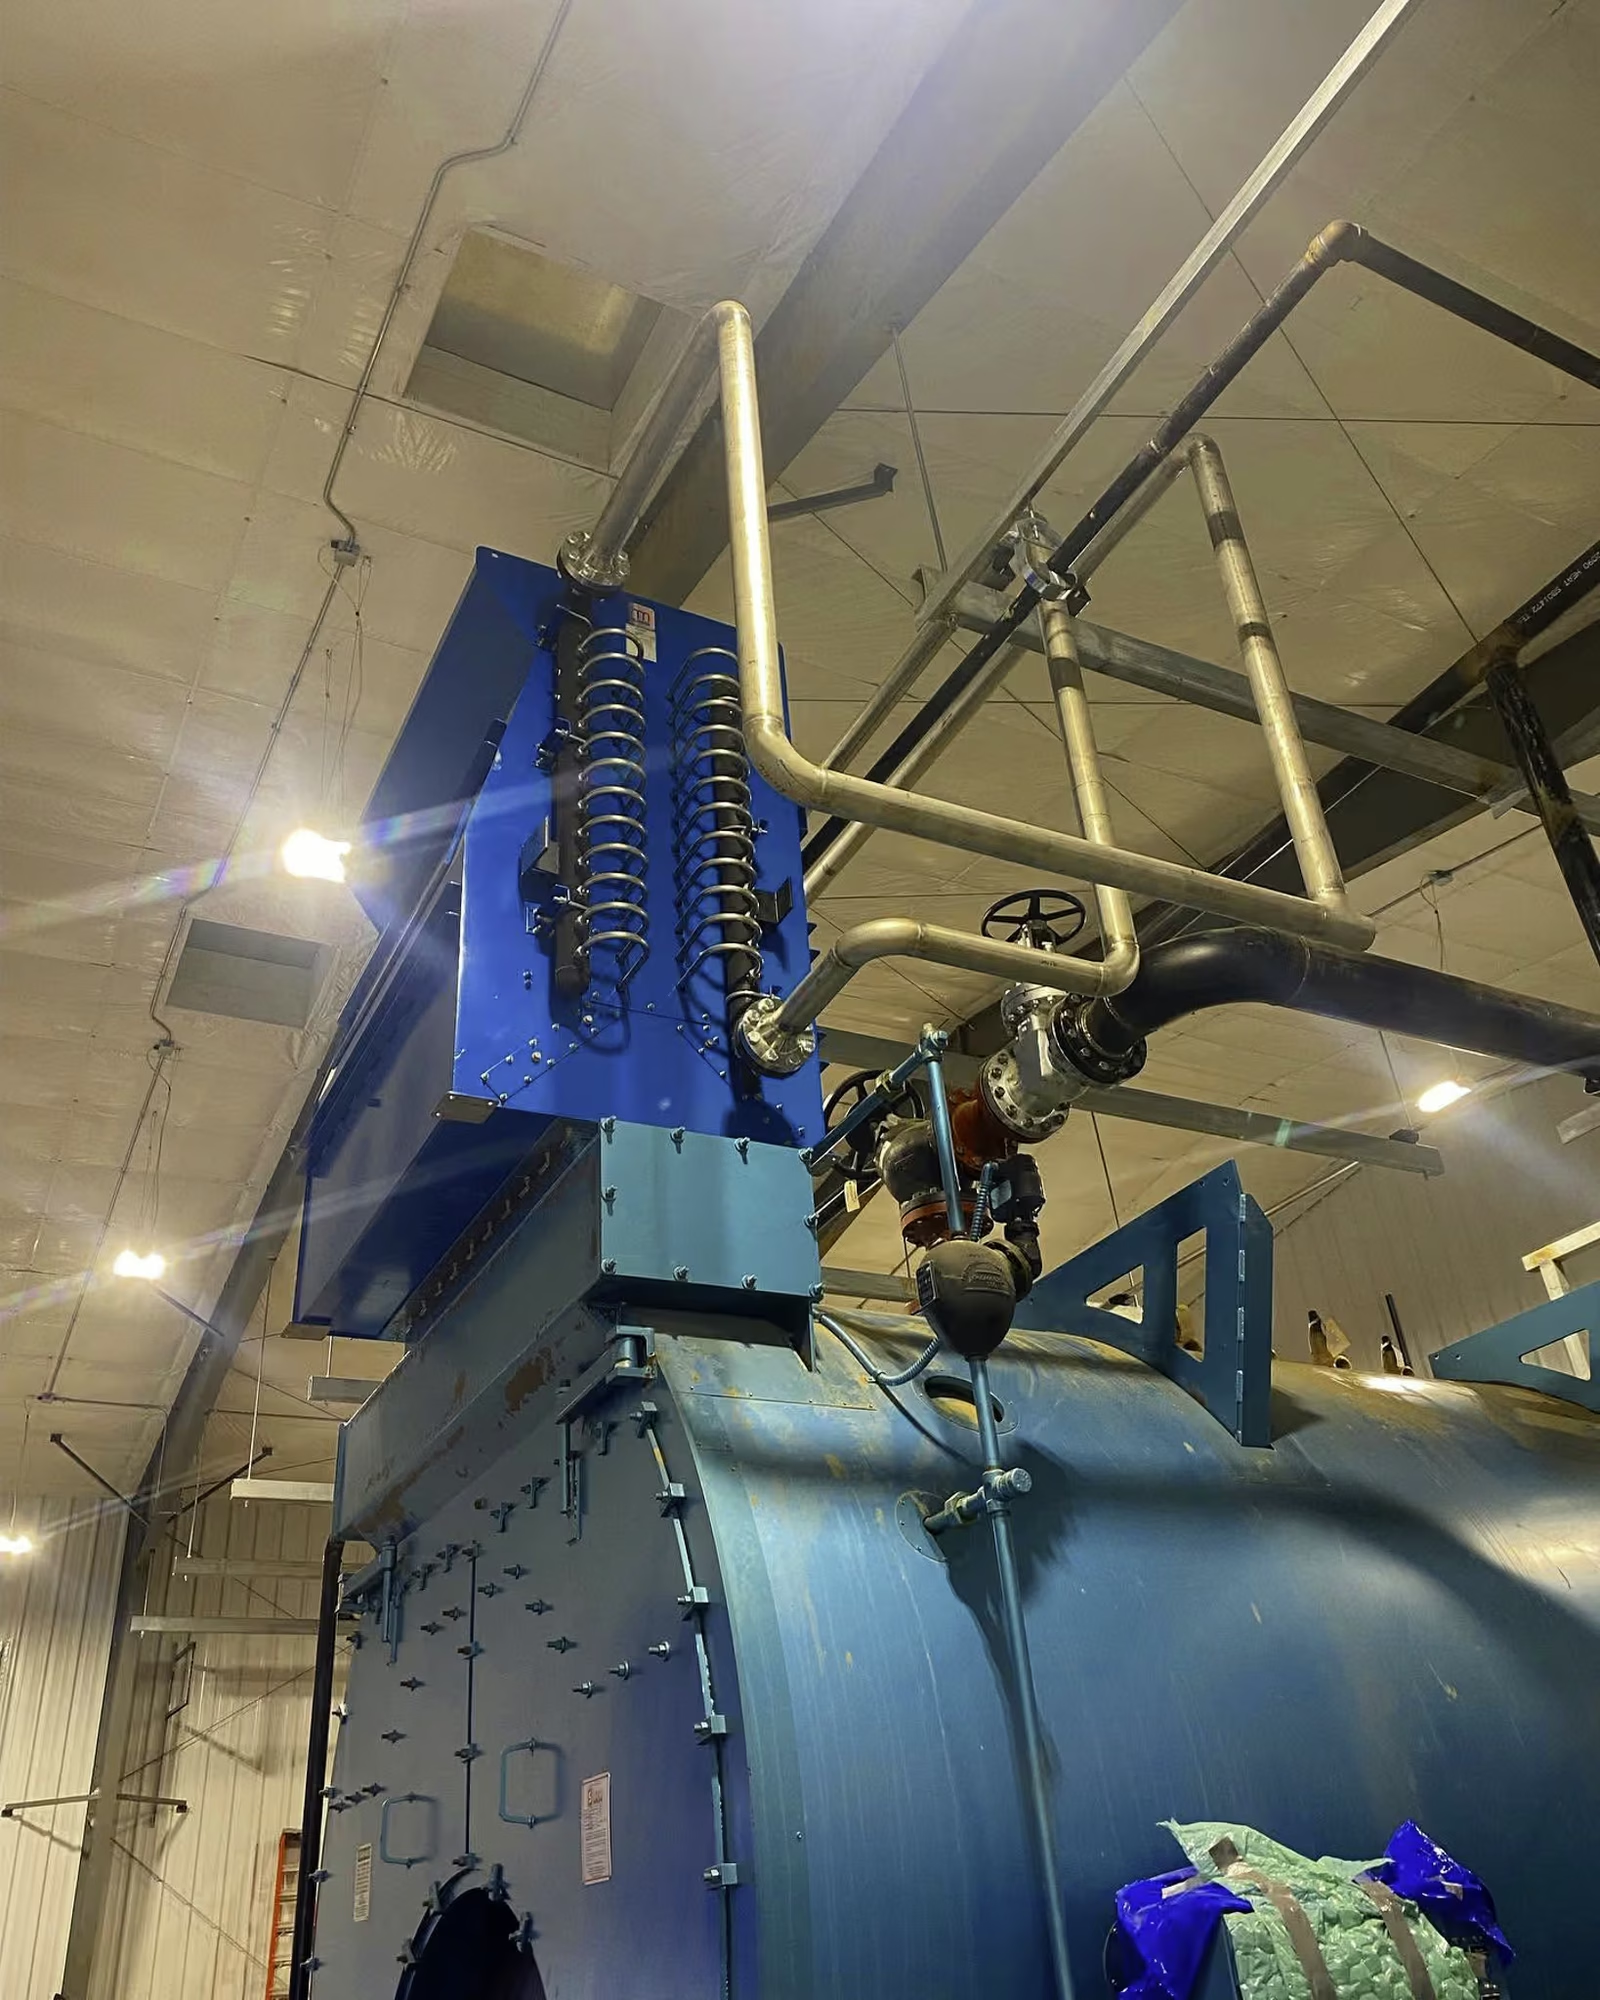
A boiler economizer is installed in the flue gas path downstream of the boiler. Hot combustion gases pass across a heat exchanger before exiting through the stack. That recovered heat can then be used to raise the temperature of boiler feedwater, make-up water, process water, or another fluid in the facility. By increasing the incoming water temperature before it reaches the boiler, the burner has less work to do to produce steam or hot water.
HEATMIZER BOILER ECONOMIZERS
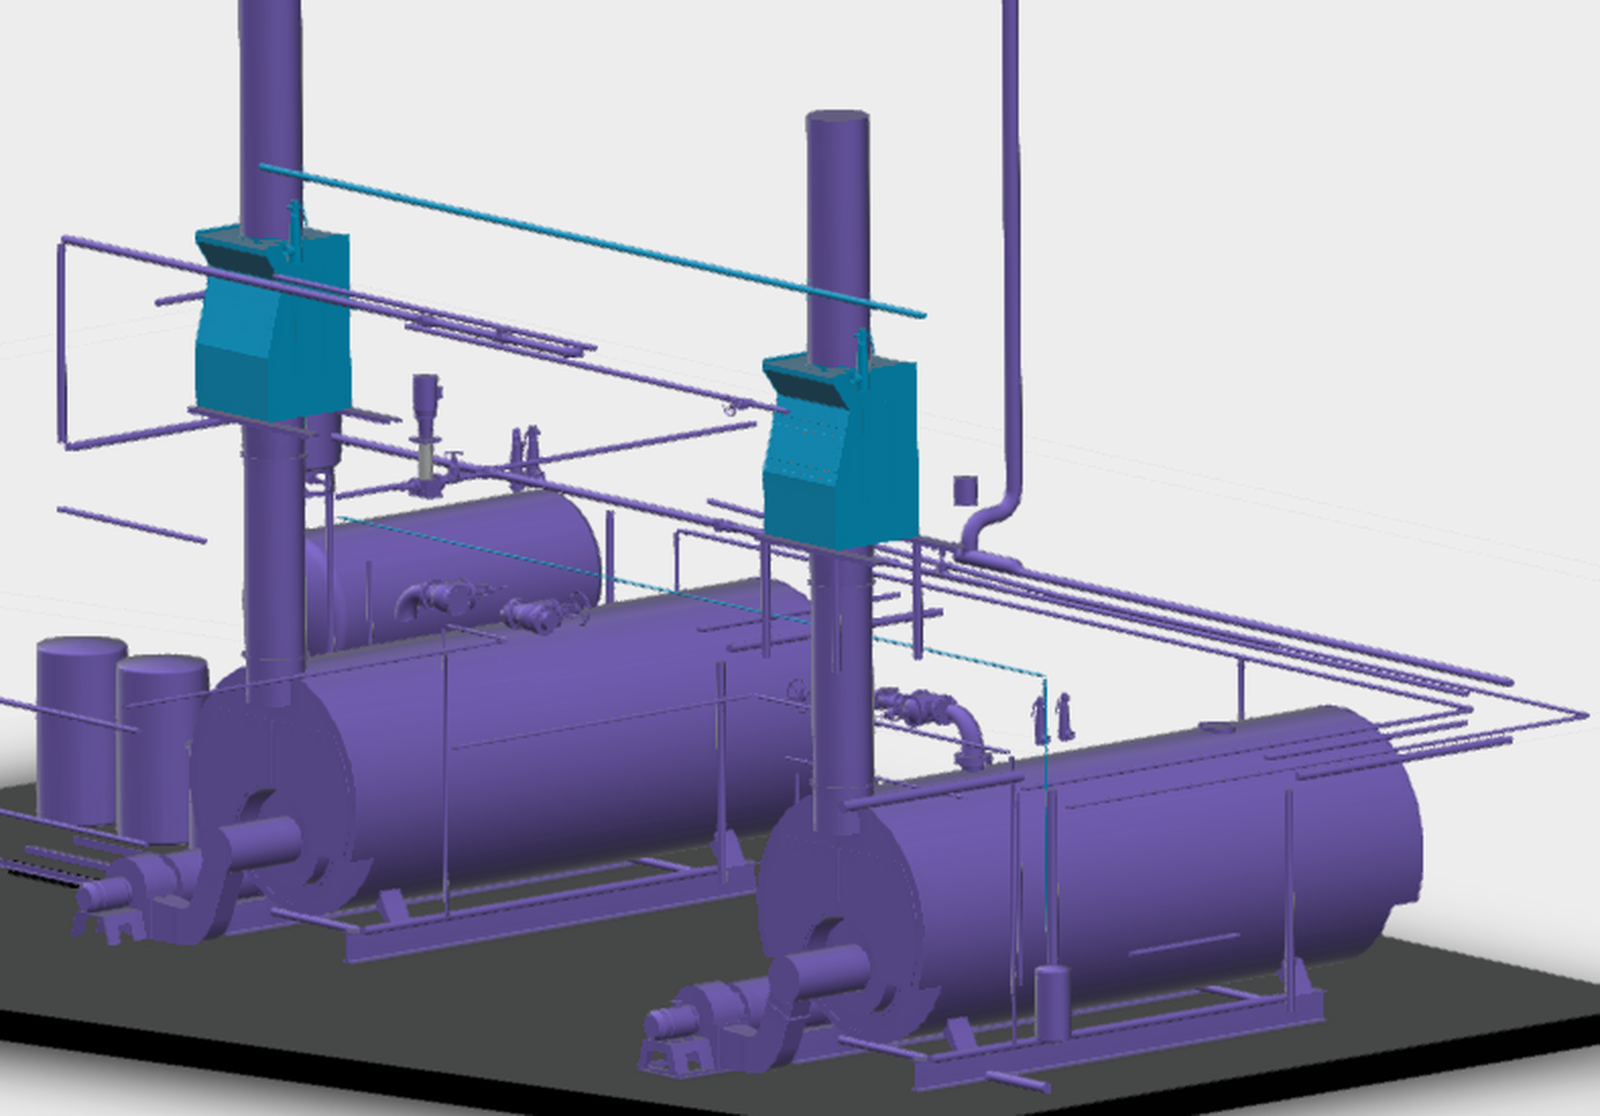
Heatmizer manufactures boiler economizers and heat recovery systems for a wide range of commercial and industrial applications. Their systems are designed around the actual operating conditions of the boiler plant, including firing rate, flue gas temperature, fuel type, water temperature, flow rate, and available pressure drop. Economizers can be configured for new boiler installations as well as retrofit applications where a facility wants to improve the efficiency of existing equipment.
Economizer Applications
BOILER ECONOMIZER PERFORMANCE
Economizer performance depends heavily on the amount of recoverable heat available in the flue gas and the temperature of the fluid being heated. Important design considerations include boiler firing rate, stack temperature, flue gas flow, inlet water temperature, water flow rate, allowable pressure drop, fuel type, and expected operating hours. The greater the temperature difference between the flue gas and incoming water, the greater the potential opportunity for heat recovery.
STACK TEMPERATURE AND HEAT RECOVERY
Flue gas leaving a boiler can still contain a significant amount of usable energy. Without heat recovery equipment, much of that energy is discharged through the boiler stack. An economizer captures a portion of that heat before it leaves the facility. Lowering stack temperature can improve system efficiency, but the economizer must also be designed to avoid operating conditions that could create condensation, corrosion, or excessive pressure drop.
BOILER ECONOMIZER RETROFITS
Facilities do not necessarily need a new boiler to take advantage of an economizer. Many existing boiler systems can be evaluated for a retrofit heat recovery system. This can be especially attractive for boilers with high annual run hours, high stack temperatures, large steam loads, or significant feedwater demand. Tri-Tech can help review the boiler operating conditions and work with Heatmizer to determine whether an economizer is a good fit for the application.
ECONOMIZERS FOR NEW BOILER SYSTEMS
For new boiler plants, the economizer should be considered as part of the complete boiler, burner, stack, and feedwater system. Coordinating the equipment early allows the economizer to be sized around expected firing conditions, feedwater temperature, available space, flue gas pressure drop, piping requirements, and system controls. This can help improve heat recovery while avoiding problems created by trying to add equipment after the boiler room has already been designed.
INDUSTRIAL BOILER ECONOMIZER APPLICATIONS
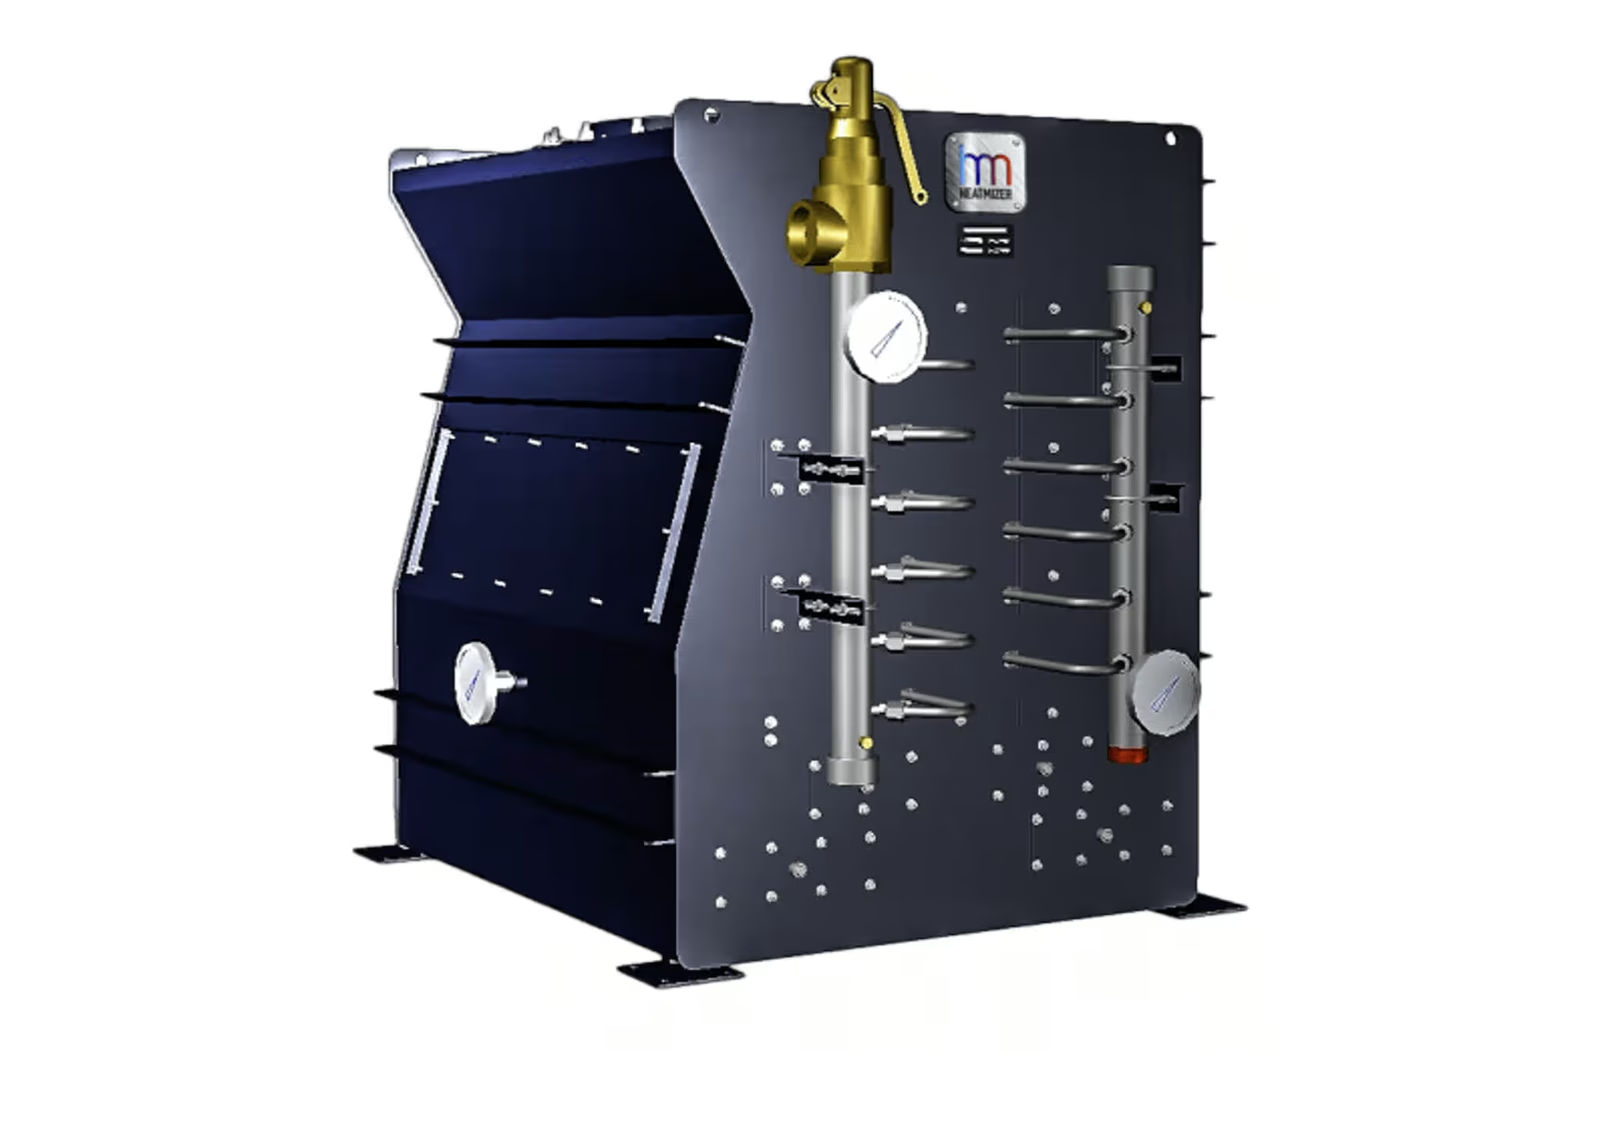
Boiler economizers can be used in facilities with significant steam or hot water demand, including manufacturing plants, food and beverage facilities, ethanol plants, healthcare facilities, universities, central plants, and other industrial operations. Applications with long boiler run hours and consistent loads often provide the strongest opportunities for energy recovery.
WHY WORK WITH TRI-TECH SALES?
Tri-Tech Sales works with commercial and industrial boiler systems every day and understands how an economizer fits into the larger boiler plant. Rather than looking at the economizer as a standalone piece of equipment, our team can help consider the boiler, burner, stack, feedwater system, operating load, and overall heat recovery opportunity. Through our relationship with Heatmizer, Tri-Tech can help customers with new economizer systems, retrofit projects, and replacement equipment.
FAST, RESPONSIVE EQUIPMENT QUOTES
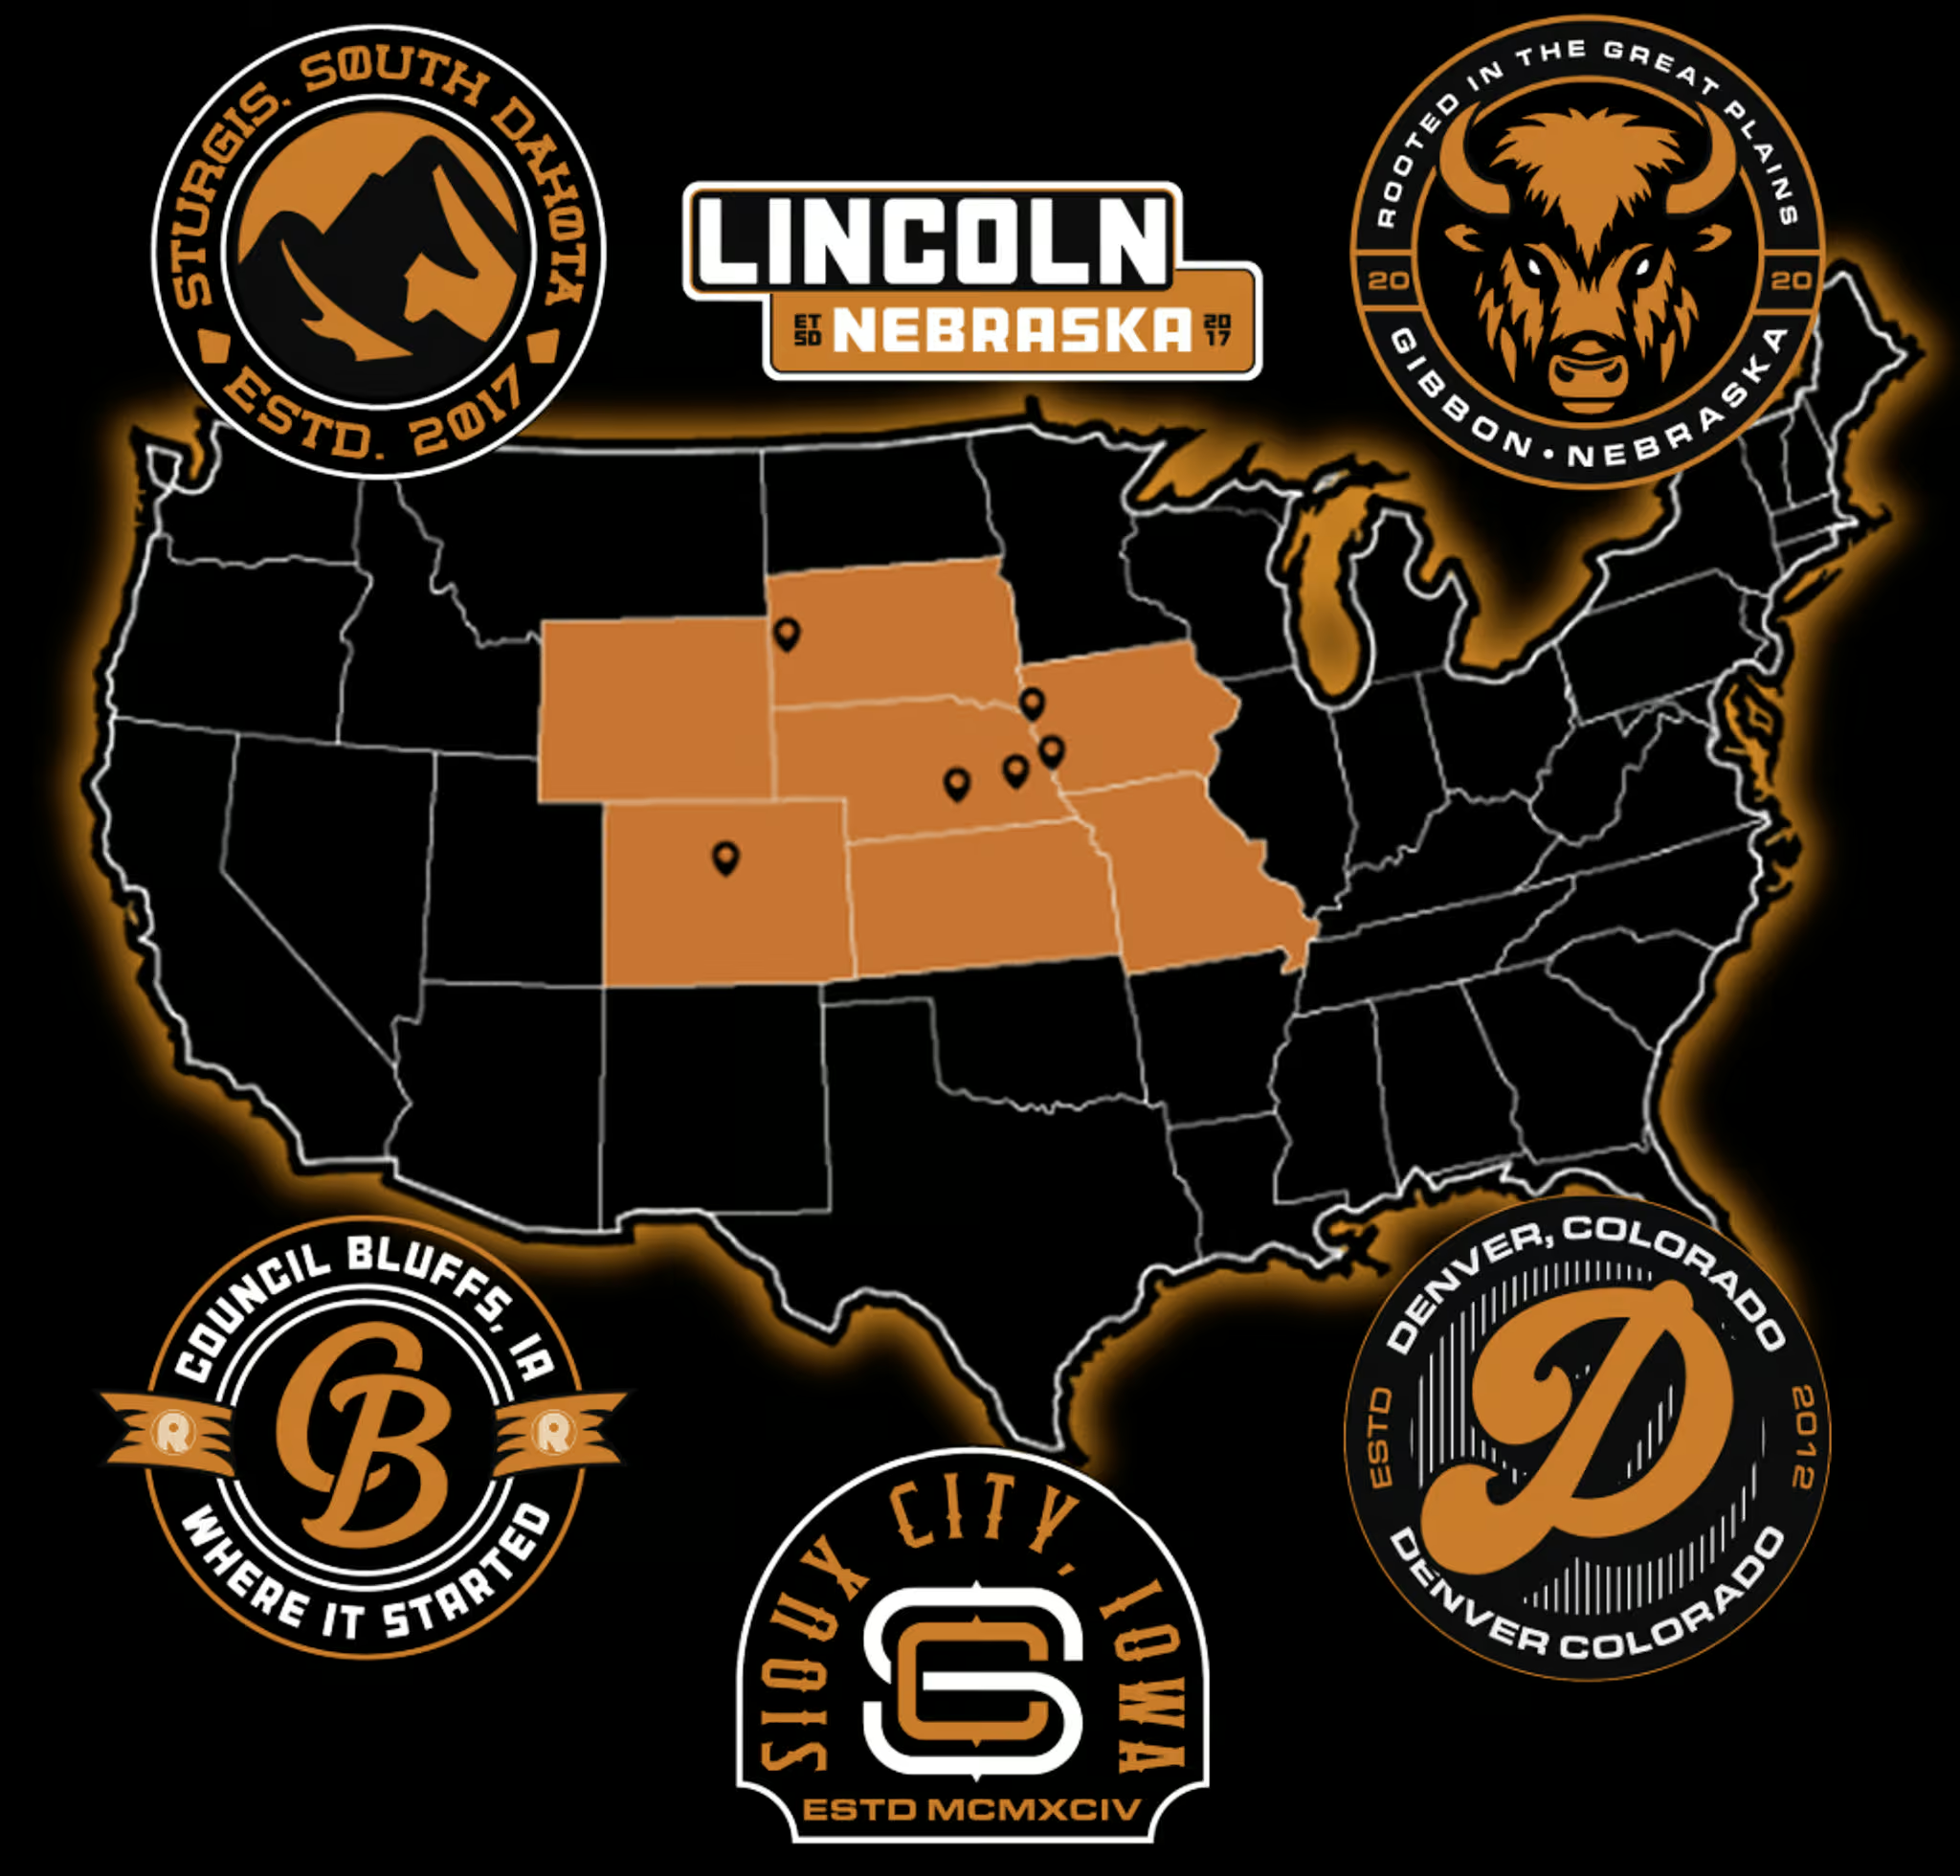
6 Locations: Council Bluffs, IA · Sioux City, IA · Lincoln, NE · Gibbon, NE · Rapid City, SD · Denver, CO
Phone: 800-874-9920
Email: support@tritechsales.com
FREQUENTLY ASKED QUESTIONS ABOUT BOILER ECONOMIZERS
What does a boiler economizer do?
A boiler economizer captures heat from flue gas before it exits the stack and transfers that heat to boiler feedwater or another fluid. This reduces wasted heat and can improve overall boiler efficiency.
How much can a boiler economizer improve efficiency?
The potential improvement depends on stack temperature, boiler load, incoming water temperature, operating hours, and system design. Facilities with high flue gas temperatures and long boiler run times generally have greater heat recovery potential.
Can an economizer be added to an existing boiler?
Yes. Many existing boiler systems can be evaluated for an economizer retrofit, provided the boiler plant has suitable operating conditions, space, piping, and stack configuration.
What information is needed to size an economizer?
Useful information includes boiler horsepower or firing rate, fuel type, flue gas temperature, operating pressure, feedwater temperature, water flow rate, and expected boiler load.
Can Tri-Tech help replace an existing boiler economizer?
Yes. Tri-Tech can review the existing economizer and current boiler operating conditions to help identify an appropriate Heatmizer replacement or upgrade.
NEED A BOILER CONDENSING ECONOMIZER?
Whether you are adding heat recovery to an existing steam boiler, replacing an aging economizer, or designing a new energy efficient boiler system, Tri-Tech Sales can help identify the appropriate Heatmizer solution for your application. Our boiler economizers are heat exchange devices that recover residual heat from exhaust gases to preheat boiler feed water or other fluid streams, improving thermal efficiency and reducing fuel costs. By capturing both sensible heat and latent heat from flue gases, including superheated steam and water vapor, economizers reduce stack temperature and heat loss, saving energy and enhancing the heat recovery process. Tri-Tech Sales offers compact design economizers made from corrosion resistant materials to withstand acid dew point and operating temperature challenges. These devices increase the temperature of cold water or boiler feed water before it enters the steam drum, reducing the fuel needed to reach the boiling point and improving overall energy efficiency. Whether retrofitting existing boilers or integrating with new power plant installations, our economizers help save energy, lower fuel consumption, and optimize heat transfer in steam turbines and other steam engine applications. Contact Tri-Tech Sales today to learn how a boiler economizer can help you preheat water supply, improve thermal energy use, and reduce heat loss in your facility.
Contact Us
Contact Tri-Tech Sales today to request information or a quote for a boiler economizer or flue gas heat recovery system.
Locations: Nebraska, Iowa, South Dakota, Colorado.
24/7 Phone: 800-874-9920
Email: support@tritechsales.com
Office Hours: Monday – Friday: 7:00am – 4:00pm